Manufacturing UK Monthly

Manufacturing UK Monthly

If you have a passion for UK Manufacturing and love to hear all the positive news about the sector we work in, then I invite you to become a member of the Manufacturing UK Monthly.

Manufacturing contributes £6.7tn to the global economy. Contrary to widespread perceptions, UK manufacturing is strong. The Manufacturing UK Monthly brings regular updates on positive news, events, best practice and articles from key people of influence all within Manufacturing.

INVITE TO JOIN THE MANUFACTURING UK MONTHLY

* indicates required


Your privacy is important to us, your details will never be shared with anyone else. Privacy & Cookie Policy

Funding for Manufacturers

Are you a Manufacturer?

Are you looking to make an improvement, solve a problem?

Would some funding help ease the costs?

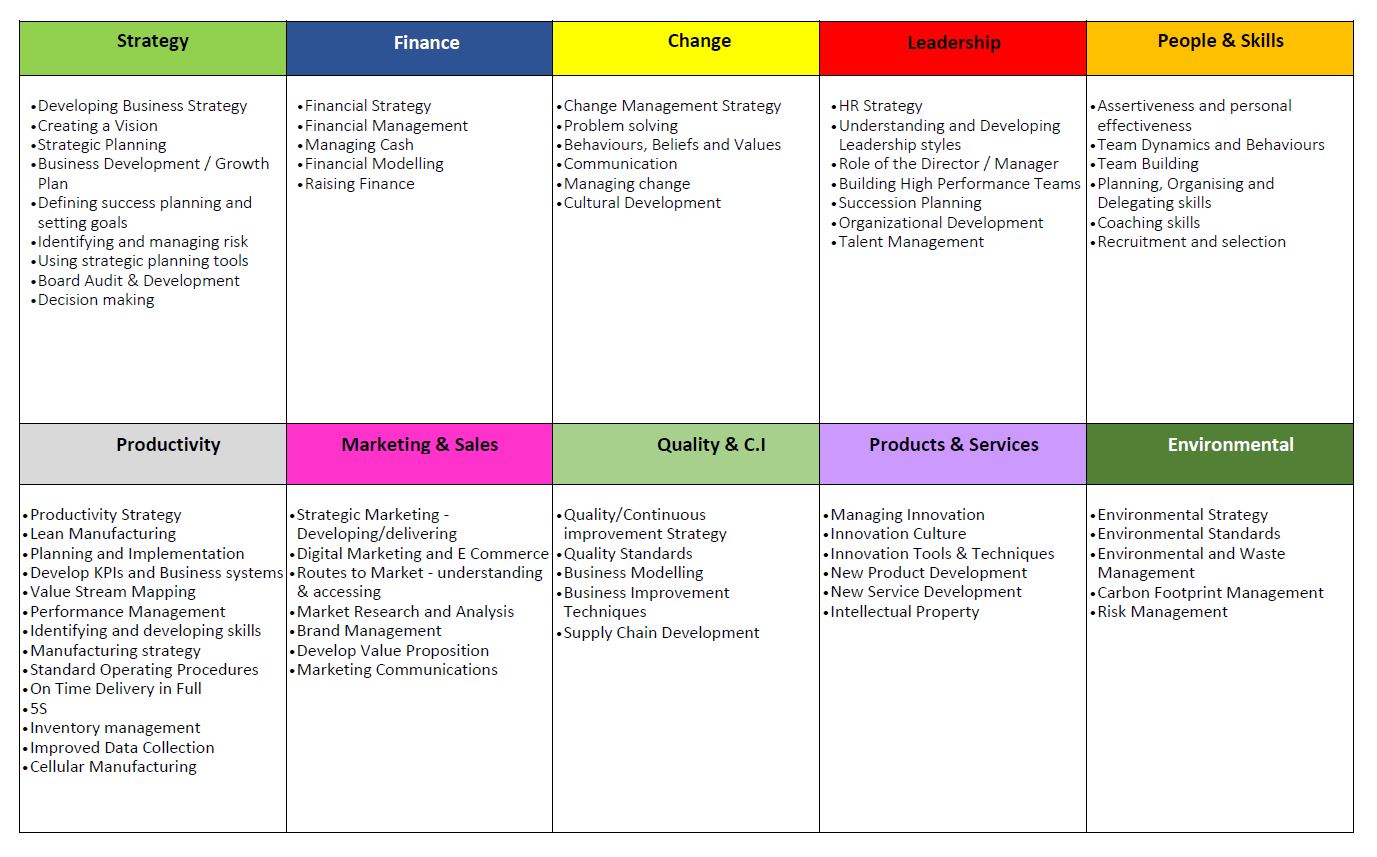
The image illustrates all interventions covered by the EDRF Funding up to September 2021. The funding covers areas including West Midlands, Yorkshire and Humber, parts of the East Midlands, South East and East of England.

(Case Study – SME Manufacturer Leverages Funding & Increases Output)

Interventions in Scope

With up to 35% grant funding our Improvement Programme is designed to stimulate the growth of aspiring manufacturing businesses, in any sector, helping them to identify opportunities for growth, solving current problems, driving continuous improvement and increasing competitive performance.

To qualify you have to be a Manufacturer with Fewer than 250 employees and a turnover less than or equal to €50 million OR a balance sheet total less than or equal to €43 million.

Just enter your name, email address and the description of the intervention you are interested in and we’ll be in touch, it’s as easy as that.

* indicates required


Your privacy is important to us, your details will never be shared with anyone else. Privacy & Cookie Policy

Automation – Don’t shy away from it.

Automation has been a cornerstone of manufacturing for years, evolving through numerous forms and innovations. This blog post delves into the significant advantages that automation, when combined with creative thinking and Lean Principles, can bring to businesses. It emphasises that while automation should not be shied away from, it is crucial to understand its impact, benefits, and justification for your business through thorough analysis.

The Evolution and Importance of Automation

Automation is not a novel concept. Its roots can be traced back to the Industrial Revolution when machinery began to replace manual labour, dramatically increasing efficiency and production capacity. Over the decades, automation has continued to evolve, incorporating advanced technologies such as robotics, artificial intelligence, and the Internet of Things (IoT). These advancements have transformed manufacturing, enabling higher precision, faster production times, and reduced human error.

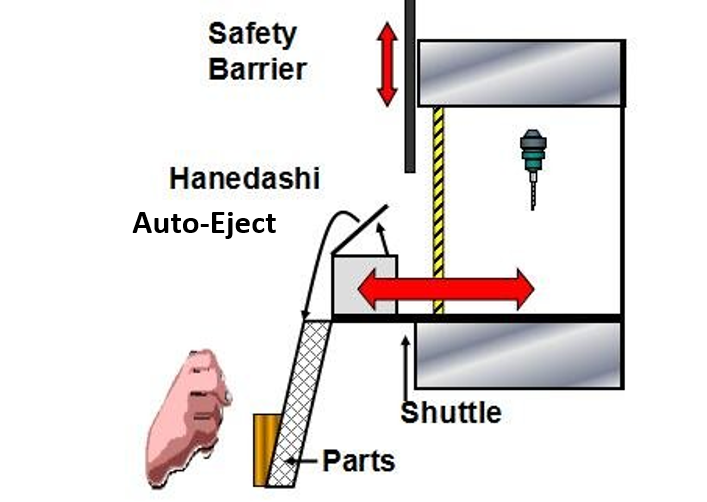
In the mid-90s, as a Kaizen Engineer with McKechnie Plc, I witnessed firsthand the transformative power of automation. We invested in machines capable of auto-ejecting or unloading parts once a cycle was completed—a process known as Hanedashi in Lean terminology. This simple yet effective device saved associate time by allowing the machine to handle the unloading process, enabling the associate to focus on loading the next part. This innovation laid the foundation for Single Piece Flow production lines, also known as Chaku Chaku Lines.

Hanedashi - Auto Eject

The Mechanics of Single Piece Flow and Chaku Chaku Lines

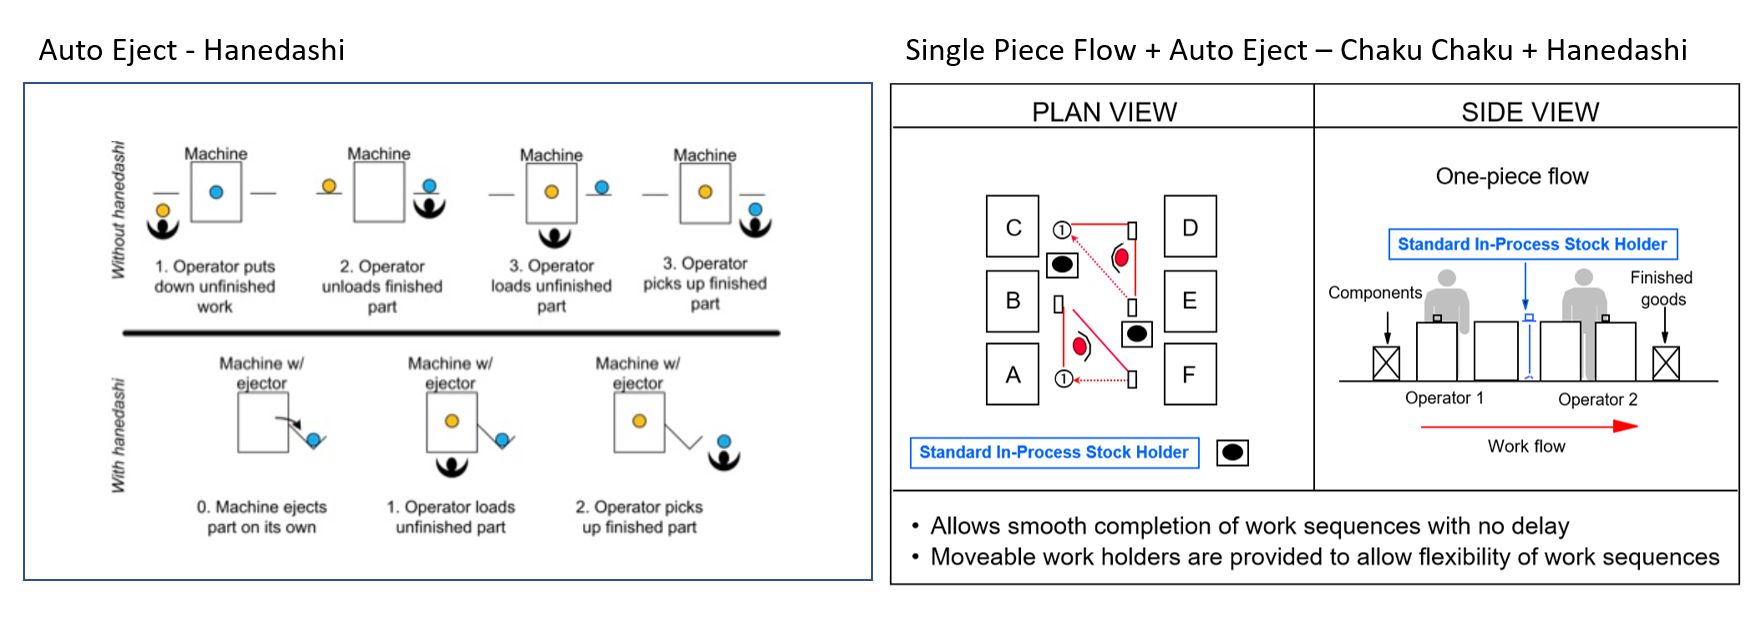
Single Piece Flow, or Chaku Chaku (which translates to “Load Load” in Japanese), is a Lean manufacturing approach where each machine in a production line is loaded with parts sequentially. All necessary machines are positioned close together, forming a cell that facilitates seamless workflow. The goal is to minimise work-in-progress (WIP) and ensure that each part moves through the production process without delays.

In a Chaku Chaku Line, automation is employed wherever possible to streamline operations. For example, loading a part into a machine may require precise orientation and proper seating in a jig, tasks that typically demand human skill. However, once the machine cycle is complete, the part can be automatically ejected, eliminating the need for manual intervention. This approach not only improves efficiency but also reduces the risk of errors and defects.

Single Piece Flow - Chaku Chaku

Jidoka: Automation with Human Intelligence

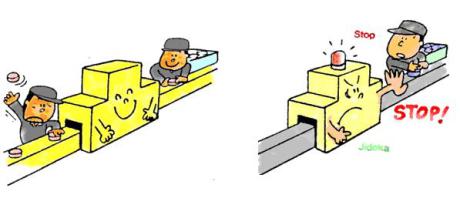
Another critical concept in Lean manufacturing is Jidoka, one of the two pillars of the Toyota Production System, along with Just-In-Time (JIT). Jidoka, often referred to as “automation with a human touch” or “autonomation,” involves integrating human intelligence into automated processes. The essence of Jidoka is to enable machines to detect and respond to problems autonomously, ensuring that production stops immediately when a defect or issue is identified.

By incorporating Jidoka, manufacturers can address the root causes of defects, leading to continuous improvements in product quality and process efficiency. This approach empowers equipment to distinguish between good and defective parts without constant human monitoring, further enhancing productivity and reducing waste.

jidoka - autnomation

Real-World Applications and Benefits

The implementation of Load Load Lines and Autonomation yields substantial benefits, including the elimination of WIP, defect-free production, and significant productivity gains. For instance, an associate can manage multiple machines simultaneously, a practice known as multi-process handling, thereby optimising labour utilisation.

In my experience at McKechnie Plc, we established a highly efficient production cell, not so creatively named Cell 7, which manufactured fasteners. The traditional production route involved multiple stages, including Header Machine, Turn, Centreless Grind, Fillet Roll, and Thread Roll, with parts moving as batches through various departments. This approach was fraught with inefficiencies and waste.
By adopting the principles of Single Piece Flow, Load Load Lines, and Autonomation, we transformed Cell 7 into a fully autonomous production line. The process began with bowl feeding fasteners into the system, after which the line handled everything else, from loading and unloading to quality inspection using visual cameras. This comprehensive automation minimised human intervention, with associates only required for machine consumables, tooling changes, and addressing any significant issues.

The Strategic Role of Automation in Modern Manufacturing

The integration of automation in manufacturing is no longer a luxury but a necessity for businesses aiming to stay competitive in a rapidly evolving market. The modern manufacturing landscape is characterised by increasing demand for customisation, shorter product life cycles, and heightened quality standards. Automation addresses these challenges by enabling manufacturers to produce high-quality products at scale, with greater flexibility and efficiency.

Customisation and Flexibility

One of the most significant advantages of modern automation is its ability to facilitate mass customisation. Advanced automated systems can be programmed to handle a wide variety of products and configurations without extensive downtime for retooling or adjustments. This flexibility allows manufacturers to meet diverse customer needs and respond quickly to market changes.

Quality Assurance

Automation also plays a crucial role in maintaining consistent quality. Automated systems equipped with sensors, cameras, and other monitoring devices can detect defects and deviations in real-time, ensuring that only products meeting stringent quality standards proceed through the production process. This capability is particularly valuable in industries where precision and reliability are paramount, such as aerospace, automotive, and medical device manufacturing.

Efficiency and Productivity

Efficiency gains from automation extend beyond the production floor. Automated systems can optimise supply chain operations, inventory management, and logistics, reducing lead times and minimising the risk of stockouts or overproduction. These improvements contribute to overall productivity and cost savings, enhancing a company’s bottom line.

Overcoming Barriers to Automation

Despite the clear benefits, some businesses remain hesitant to embrace automation due to perceived barriers such as cost, complexity, and potential job displacement. However, these concerns can be addressed through strategic planning, careful analysis, and a focus on long-term gains.

Cost Considerations

While the initial investment in automation technology can be substantial, the long-term benefits often outweigh the costs. Businesses should conduct a thorough cost-benefit analysis to assess the potential return on investment (ROI). Factors to consider include increased production capacity, reduced labour costs, improved quality, and shorter cycle times. In many cases, the savings and efficiencies gained through automation can lead to a rapid ROI.

Skill Development and Workforce Transition

Another common concern is the impact of automation on the workforce. While automation can reduce the need for certain manual tasks, it also creates opportunities for new roles that require advanced technical skills. Companies can mitigate job displacement by investing in training and development programs to upskill their employees, preparing them for higher-value tasks such as programming, maintenance, and quality control.

Complexity and Integration

Integrating automation into existing processes can be complex, particularly for businesses with legacy systems. However, advancements in technology have made it easier to implement and integrate automated solutions. Collaborative robots (cobots), for example, are designed to work alongside human operators, enhancing productivity without the need for extensive modifications to existing workflows. Additionally, modular automation systems can be scaled and adapted to meet evolving needs.

The Future of Automation in Manufacturing

The future of manufacturing is undeniably intertwined with the continued advancement of automation technologies. Emerging trends such as Industry 4.0, the Industrial Internet of Things (IIoT), and artificial intelligence (AI) are set to further revolutionise the sector.

Industry 4.0 and the Smart Factory

Industry 4.0 represents the fourth industrial revolution, characterised by the integration of digital technologies into manufacturing processes. This paradigm shift encompasses the use of IoT devices, data analytics, and AI to create smart factories where machines communicate and collaborate autonomously. These connected systems enable real-time monitoring, predictive maintenance, and data-driven decision-making, leading to unprecedented levels of efficiency and flexibility. This is something our sister company offers FactoryIQ – The Smart Factory Made Simple

Artificial Intelligence and Machine Learning

AI and machine learning are poised to play a transformative role in manufacturing automation. These technologies can analyse vast amounts of data to identify patterns, optimise processes, and predict potential issues before they occur. For example, AI-driven predictive maintenance can significantly reduce downtime by identifying when equipment is likely to fail and scheduling maintenance proactively.

Collaborative Robotics

Collaborative robots, or cobots, are designed to work safely alongside human operators, enhancing productivity and flexibility. Cobots can handle repetitive, hazardous, or ergonomically challenging tasks, allowing human workers to focus on more complex and value-added activities. As cobot technology advances, their capabilities and applications will continue to expand, making them an integral part of the modern manufacturing landscape.

Additive Manufacturing

Additive manufacturing, commonly known as 3D printing, is another technology that complements automation. It enables the production of complex and customised parts with minimal waste and reduced lead times. When integrated with automated systems, additive manufacturing can streamline prototyping, reduce inventory costs, and accelerate product development cycles.

Case Study: Transforming Manufacturing with Automation at McKechnie Plc

To illustrate the impact of automation in a real-world setting, let’s revisit the case of McKechnie Plc, where I worked as a Kaizen Engineer in the mid-90s. Our journey with automation began with the introduction of Hanedashi devices, which automated the unloading of parts from machines. This initial step laid the groundwork for more extensive automation initiatives.

Setting Up Single Piece Flow and Load Load Lines

Recognising the potential of Single Piece Flow, we restructured our production lines to create Chaku Chaku Lines. By co-locating all the machines needed for a product in a single cell, we minimised the time and effort required for material handling. Automation played a crucial role in this transformation, with machines automatically ejecting finished parts and readying themselves for the next cycle.

Implementing Autonomation for Quality Assurance

To further enhance our production process, we integrated Jidoka principles, enabling machines to autonomously detect and respond to defects. Visual cameras were installed to inspect parts in real-time, ensuring that only high-quality products moved forward in the production line. This autonomation approach not only improved product quality but also reduced the need for manual quality checks, freeing up associates to focus on other tasks.

Achieving Full Autonomy with Cell 7

Cell 7, our fastener manufacturing cell, became a showcase of automation excellence. By combining Single Piece Flow, Load Load Lines, and autonomation, we achieved a fully autonomous production process. Fasteners were bowl fed into the system, and the line handled everything from loading and unloading to quality inspection and defect rejection. Human intervention was required only for machine consumables, tooling changes, and addressing significant issues.

Results and Benefits

The results of our automation efforts were nothing short of remarkable. We experienced a significant reduction in work-in-progress, virtually eliminating delays and bottlenecks. Product quality improved dramatically, with defects identified and addressed in real-time. Productivity soared as associates could manage multiple machines simultaneously, optimising labour utilisation. Overall, the integration of automation led to substantial cost savings, higher efficiency, and enhanced competitiveness.

Conclusion: Embracing Automation for a Competitive Edge

Automation, when combined with creative thinking and Lean Principles, offers immense benefits to businesses. From improving efficiency and productivity to enhancing product quality and flexibility, the advantages are clear. However, it is essential to approach automation strategically, conducting thorough analysis to understand its impact and justify the investment.

As the manufacturing landscape continues to evolve, staying ahead of the curve requires embracing automation and leveraging advanced technologies. By doing so, businesses can unlock new levels of performance, reduce costs, and remain competitive in an increasingly dynamic market.

At TCMUK Limited, we are committed to helping UK manufacturers embed strategies that reduce costs, increase sales, and boost profits. Our expertise in automation and Lean Principles enables us to guide businesses through the complexities of implementing and optimising automated systems. Whether you are looking to enhance your existing processes or embark on a comprehensive automation journey, we are here to support you every step of the way.

If you are ready to explore the transformative potential of automation for your business, contact us today to learn more about our services and how we can help you achieve your goals. Don’t shy away from automation—embrace it and unlock the full potential of your manufacturing operations.


0330 311 2820

Improve Productivity

Copy and Deploy the ultimate productivity swipe file to reduce costs and increase efficiency of your processes.

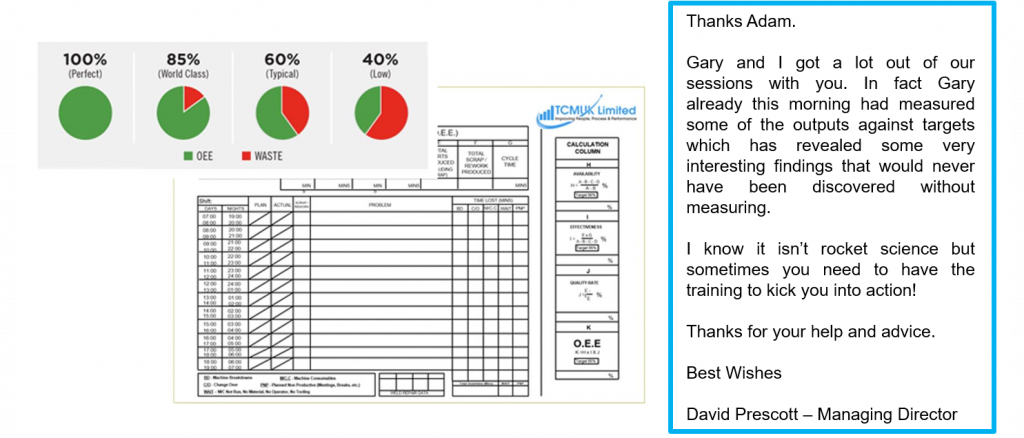
OEE (Overall Equipment Effectiveness) is a “best practices” metric for monitoring and improving your manufacturing processes (i.e. machines, cells, production lines…). OEE is simple, practical and powerful. It takes the most common sources of manufacturing productivity losses and places them into three categories: Availability, Performance and Quality.

This swipe file will help in understanding the data required to monitor your machines and manufacturing processes in shifting towards IR4.0 and taking the next step in fully automating the data collection.

For further reading on OEE “click here”

OEE - Improve Manufacturing Productivity

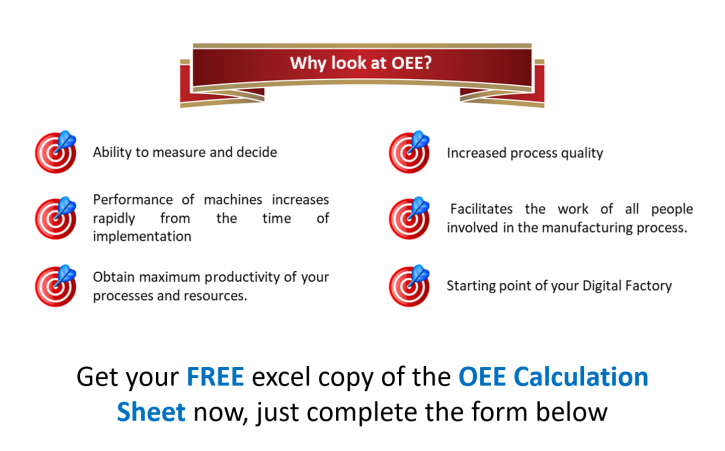
Benefits of OEE

* indicates required


Your privacy is important to us, your details will never be shared with anyone else. Privacy & Cookie Policy

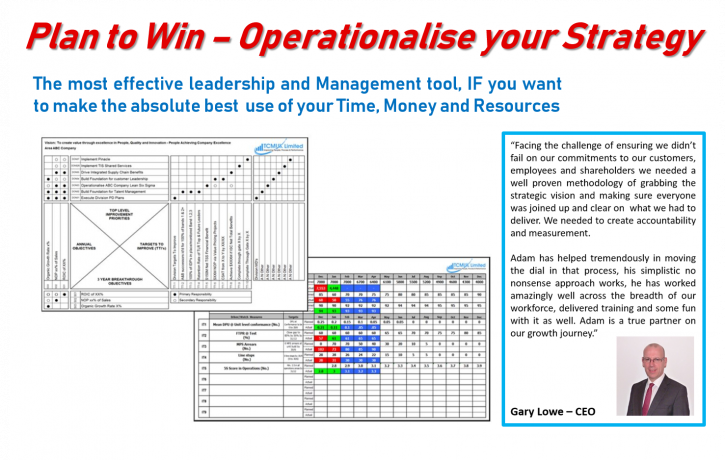
Operationalise your Strategy – FREE Download

OOperationalise your Strategy
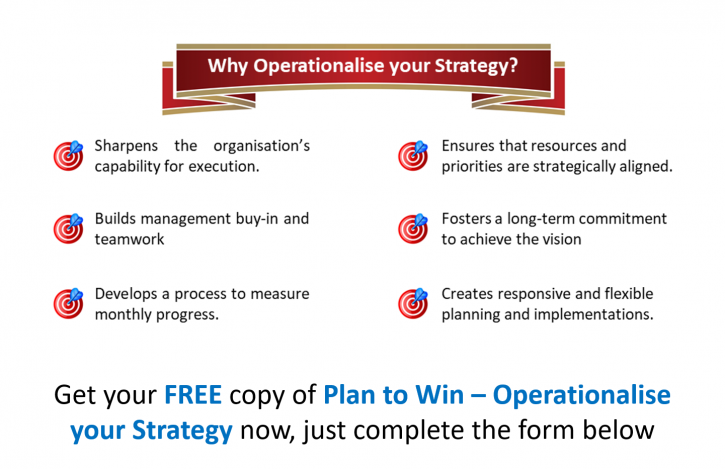
Benefits of Policy Deployment

Organisations with the capability to consistently execute their plans through the adoption of Strategy Execution outperform the market. Forget all the meaningless buzzwords and fancy dashboards, you need context and a trackable action plan to drive real performance improvements.

* indicates required


Your privacy is important to us, your details will never be shared with anyone else. Privacy & Cookie Policy

Sales and Operations Planning – is it a missing link in your business???

Benefits of Sales and Operations Planning

  • Increased customer service levels
  • Improved profitability
  • Reduced time to market with new products
  • More products to increase revenue
  • Lower inventories and obsolescence
  • Reduced lead times
  • Quicker responsiveness
  • Top-down management control
  • Predictable operating performance for shareholders

The Sales and Operations Planning process is the primary tool by which there is a systematic review of the business, out of which plans are established. It brings Sales, Marketing, Manufacturing and Finance together to agree on the volume of products to be produced over the next sales horizon. The process should be incorporated into the business calendar to coincide with the key activities of, strategic reviews, budget preparation, quarterly forecasting, monthly performance reviews and MRP/ERP timing.

Alignment from S&OP Process goes beyond just the meeting, the entire company is aligned to a given direction. This is one of the huge benefits from the S&OP Process. The Master Scheduler is implementing the decisions made by the S&OP team. The planners and buyers are aligning to the Master Scheduler. Capacity is being increased and decreased in accordance to the plan. Changes to the financial plan are made in advance given the decisions from the S&OP meeting. The monthly meeting allows for issues to be raised, tracked and resolved. Key department heads are present so that the entire company can be aligned behind a decision and as it is cascaded and communicated to the levels below.

The sales and operations plan looks 12 – 18 months into the future, this level of visibility opens the door to a different way of thinking: a longer term view. The process facilitates the bringing together of data from different departments and presents it to the team (Operations has visibility to Sales plans. Sales have visibility to the supply plan. Finance has visibility to expected revenues and expenses)

Finance are an integral part to making the process successful, they ensure the alignment of the financial plan to the operational plan so ultimately the objective of making money is achieved and on track. It’s no good planning to ramp up 30% if you only have the resources to ramp up 10%.

New product introduction (NPI) can be a headache (new suppliers, ramp up, technical issues, capacity, obsolete inventory, etc) but again the S&OP process facilitates the discussion. It enables all stakeholders to be aware when a new product introduction is happening. Sales needs to be talking to Operations. Operations needs to be talking to Finance. Many companies deal with NPI separately and have a project plan dealing specifically with new product introductions With NPI on the agenda within the S&OP process, issues can be raised, actioned and tracked, (releasing of capacity for trials, product traceability, etc) are managed carefully.

A big part of the S&OP agenda is reviewing the key business metrics in order to identify and resolve performance issues, when issues are raised, the key stakeholders are in the room to get things done.

0330 311 2820

Book a Return Call at a time that Best Suits You “HERE”

The saying goes “Culture eats Strategy for Breakfast” Drucker

The weekend of October 22nd I was watching the Austin Texas F1 Grand Prix, this is one programme that everyone knows in my house not to disturb me watching. This weekend Mercedes were all but clear of winning the constructors championship as long as Ferrari didn’t outscore them by 17 points, something in the end that Ferrari couldn’t do. Congratulations MercedesAMGF1!

Now what pricked my ears up was the interview with James Allison at the end of the race, a number of questions were asked around the differences between Ferrari and Mercedes, James (Ferrari man from 2000-2005 and returning 2013-2016 to Mercedes 2017) an absolute professional and held in high regard within F1 would not be drawn on the comparison, but what he did say regarding Mercedes summed it up in 28 seconds of video (click the image below for the interview).

If you look at Ferrari’s take on things in the past few races when things have been going wrong, their behaviour seems to be one of blame and bullet a few people, you would almost say “Manage by Fear”.

As James Allison put, by being Brave to Ultimately Prosper and the culture they have embedded at Mercedes to succeed clarifies the saying “Culture eats Strategy for Breakfast”

Culture is hard to collate, classify, categorise and it’s certainly hard to measure, it also seems one of those things Businesses seem to shy away from, even borderline not accept. It’s the invisible glue that you can’t touch or feel, so we’ll ignore it.

BUT IGNORE IT AT YOUR OWN RISK THOUGH!

Quite often, businesses think culture is some flowery-fluffy stuff that doesn’t make any difference in the end, or even if they think it does matter, they have an excruciatingly hard time describing what theirs is.

This invisible glue that holds the organisation together is probably the most powerful entity you can tap into, it’s part of your businesses DNA, the same as how I describe Policy Deployment, it becomes part of your business DNA. The “How you get things done”

The “How you get things done” drives performance.

Culture is not what we say, but what we do without asking. A healthy culture allows us to produce something with each other, not in spite of each other. That is how a group of people generates something much bigger than the sum of the individuals involved.

So don’t underestimate “YOUR BUSINESSES CULTURE”

0330 311 2820

Book a Return Call at a time that Best Suits You “HERE”
Operationalise Your Strategy

Benefits of Policy Deployment

  • Organisations with the capability to consistently execute their plans through the adoption of Strategy Execution outperform the market.
  • Organisational capabilities will be aligned to support the achievement of your company objectives.
  • Resources will be allocated to business processes in priority order (according to the importance/contribution the process makes to your business)
  • Your company can excel in the business/commercial sector in which it operates.

The Policy Deployment process has yielded some unbelievable benefits for me in my career and it’s one of those processes I recommend all businesses leaders introduce, (but I will also state if you are not prepared to apply the rigorous PDCA management process that goes with it, it’s not for you). I’ve been using Policy Deployment for 15+ years across multiple businesses, as an example: £1bn Turnover business, achieving £200m EBITDA across 38 sites globally, including Lean Savings within the first year of £21m. Done well, it works!

Some of you are probably getting to the stage or are currently producing budgets for your coming year. Now wouldn’t it be worthwhile aligning your Strategy and your budget requirements and drive some break through thinking into the process.

The process itself comes from a technique called Hoshin Kanri, which is a method devised to capture and cement strategic goals, well for me it does more that cement goals, it disseminates those goals into tactical projects that are owned, timed bound and measured.

There have been a number of English translations Policy Deployment, Goal Deployment, Hoshin Planning. I prefer Policy Deployment Process or PDP, but as you probably know from me by now, call it what you want just as long as you use it.

So What DOES it do?

  • It forces the clear identification of “How” we move ourselves towards our Strategic objectives.
  • It creates an alignment of all facets of the organisation on the key strategic initiatives (cross-functional teamwork).
  • Fosters a data-oriented, fact-based culture.
  • Reinforces the vision, but also clearly defines how we will get there (Based on “Who” does “What”).

What it DOESN’T do!

  • Achieve results if the management process isn’t changed (Moved to rigorous PDCA).
  • Achieve results if the “How’s” (Improvement Priorities) aren’t the right ones.
  • Achieve results if the “How’s” aren’t clearly defined.
  • Replace the need for solid Business Fundamentals (also known as Daily Management).

The process is intended to help an organisation:

take the Company Vision (desired end state, aspirations, business scope); the Strategy (3-5 Year Strategic gaps/objectives, high level plans for competitive advantage) and creates a One year distillation of these 3-5 year objectives.

It creates improvement priorities and metrics for tracking progress and indicates the resource responsible and accountable for them. A tactical implementation project if you like (you can go further with the process and state which projects need to be completed within each quarter of the year, to add additional focus).

Detailed action plans (A3’s) are produced for each one of the improvement priorities and reviewed on weekly/monthly/quarterly basis through monitoring of the PDP metrics.

These reviews should be held by a cross functional team who challenge each other, learn from each other and drive execution of the improvement priorities.

Typical Strategy Objectives may be:

  • Double Top Line Sales in 5 yrs
  • Double OP % to Sales in 3 yrs
  • Reject PPM Reduction by 90% in 3 yrs
  • Reduce Lead-time by 75
  • On Time Delivery to 100% in 3 yrs

Typical Annual Objectives may be:

  • Grow Top Line Sales by 15%
  • Increase OP by 25%
  • Reject PPM Reduction by 50%
  • Reduce Lead-time by 50%
  • OTD +20%

Improvement Priorities may be:

  • Quality: Create & Implement Rapid Defect Reduction Process, Implement DFSS on Critical Products
  • Delivery: Apply Lean ‘Tools to XYZ to Reduce LT, Implement Back-Office LT Reduction Process
  • Cost: Develop & Implement LCR Sourcing Plan, Launch Productivity Improvement Std Work Series in Assembly

So Why Use it?

97% of Businesses have a Vision
80% have a clear Strategic Plan
52% some Execution/Success
33% Significant Execution Success
Where do you think Policy Deployment is having an Effect?

0330 311 2820

Book a Return Call at a time that Best Suits You “HERE”

Key Performance Indicators – Always an Emotive Subject

You may have seen my recent post if you follow me on linkedin regarding measuring Production Output with Value (£). With over 11000 views and numerous comments, this got me thinking about KPIs (key performance indicators) and business.

KPIs drive behaviour (no doubt in that) getting the wrong KPI can have a massive negative impact, the image below sums it up, wrong KPI with Targets = Lost at Sea, Wrong KPIs and No Targets = Shipwreck.

A good KPI should act as a compass, helping you and your team understand whether you’re taking the right path toward your strategic goals.

KPIs are key for any business and impact on a number of facets,

  • TO COMMUNICATE STATUS – ACTUAL v TARGET
  • PLANT LEVEL
  • BUSINESS LEVEL
  • WORK STATION LEVEL
  • TO DRIVE IMPROVEMENT BY FACT NOT GUESSWORK
  • TO HELP PRIORITISE IMPROVEMENT ACTIVITY
  • A CONTINUAL HEALTH CHECK FOR THE BUSINESS
  • TO CONNECT THE CUSTOMER TO THE PROCESS (something that gets forgotten)

One of the best ways to understand and align your KPIs is through generating a KPI tree, a KPI tree has 2 main purposes:
To clarify the responsibility (at each level) to ensure achievement of the correct result or activity that will deliver the Company’s and Customers goals, objectives and values.
Definition of responsibility: The responsible level is the lowest level that has the authority and the ability to 100% achieve the required result or activity.
To clarify the link between each result and activity to ensure appropriate prioritisation of activities

The KPI tree structure is separated into four different categories, these are as follows –

High level KPI – The key measure which drives achievement of the Company and Customer goals, objectives and values
Result KPI – The management tool used to measure the effectiveness of the activities completed to support the achievement of the goals and objectives
Activity KPI – The enabler to improve the current situation. (What you can see you can fix)
Activity – Either the physical actions taking place at any level in order to achieve the goals or the understanding of the current situation by Go Look See

Here’s a typical example of a KPI tree for “Delivery”

0330 311 2820

Book a Return Call at a time that Best Suits You “HERE”

Get your Changeovers out of the Slow Lane

Why long set ups quietly cap your capacity, and how SMED gets the time back without buying another machine.

There’s a conversation I’ve heard in more factories than I can remember. A key machine is “at capacity.” A customer’s getting nervous. Somebody puts a quote for a second machine on the MD’s desk, and the talk turns to finance, floor space and who on earth is going to run it.

And nobody, at any point, asks how much of the week that first machine actually spends making parts.

Whether you run a high-volume business or a low volume one, changeovers are one of those things that can quietly drain the life out of your manufacturing process. Left alone, an unstructured approach to set ups has a habit of growing arms and legs. Then the arms and legs grow arms and legs. Nobody plans it. It just creeps.

I first saw this properly in the early nineties. I was a Kaizen engineer at a business making aerospace fasteners, and we were being trained in lean manufacturing by a Japanese sensei. He split us into three teams for a week of improvement events on three different machines: a centreless grinder, a thread roller and a header machine. My team got the header.

The first thing we did was film a real changeover, start to finish. Not a demonstration. The real thing, done the way it had always been done.

When we added it up, there were eight hours of it. A whole shift. For a production run that would last thirty minutes to an hour, depending on batch size, and we were talking batches in the thousands. The machine ran three shifts, so a big slice of its working life was spent getting ready to work.

And here’s the bit that still makes me smile. A major customer had flagged that machine as a high risk to their supply because of capacity. They were actively pushing us towards buying another one.

At the start of the week, we’d have been delighted with a 50% reduction. Honestly, that felt ambitious. Never in a million years did we think we’d get it under thirty minutes. But we did.

That week changed how I look at every factory I walk into. So this post is the longer version of what I learned, brought up to date for UK manufacturing in 2026. What long changeovers really cost you, why you should film one before you touch anything, how to split internal work from external work, and the three words that have stuck with me for over thirty years: eliminate, combine, simplify.

What a long changeover is really costing you

Most people think of a changeover as lost machine time. It is. But I think that’s the smallest part of the bill.

The bigger cost is what long changeovers force you to do to cope with them. If a set up takes half a shift, nobody wants to do it often. So you run bigger batches. Bigger batches mean more work in progress on the floor, more finished goods in the stores, more cash tied up in stock and more floor space lost to racking. You make things before anybody’s ordered them, which is overproduction, the waste that tends to feed all the others. Jobs wait in a queue behind the big run. Material gets moved, stacked, then moved again. Lead times stretch, so you quote longer, so customers order earlier and in bigger lumps, and round it goes.

In other words, a long changeover doesn’t just waste an hour. It sets your batch size. And your batch size quietly sets your stock, your lead times and a fair bit of your cash flow.

There’s a nice bit of history here. For most of the twentieth century, factories worked out batch sizes using the economic order quantity, a formula that treats set up time as a fixed cost you simply have to live with. Toyota’s big insight was to question the “fixed” part. If changeovers get short enough, the economic batch gets small, and suddenly you can make what customers actually want, when they want it.

That matters more for UK manufacturers now than it did when I was stood next to that header machine. A lot of your customers want smaller quantities, more variants and shorter lead times, and they don’t want to pay for you holding their stock. For plenty of UK firms, high mix, low volume isn’t a niche anymore. It’s just the work.

Then there’s capacity. Make UK’s Q3 2026 Manufacturing Outlook showed the UK orders balance rising from +12% to +17%, but manufacturers holding back on hiring because employment, energy and input costs are still biting. More orders. Same people. Same machines. So where’s the extra output meant to come from?

Before you sign off a second machine, or another shift you can’t staff, it’s worth asking a slightly awkward question. How much capacity is already sitting inside your changeovers, waiting to be found?

In my experience, it’s usually more than anyone guesses. Quite a lot more.

Film it before you fix it

If you take one thing from this post, make it this. Before anyone suggests a single improvement, film a real changeover.

Not a rehearsed one. Not the one your best setter does when he knows the MD’s watching. The normal one, on a normal day, from the last good part of the old job to the first good part of the new one. That’s the bit that counts, by the way. The changeover isn’t finished when the new tool’s in. It’s finished when you’re making good parts at the right rate.

Why video? Because memory is hopeless at this. Ask a setter how long a changeover takes and you’ll get an honest answer that’s often wildly out, because nobody notices the walking, the waiting and the searching. They just feel like part of the job.

When you play the footage back with the team, a few things almost always jump out.

Walking. One practitioner wrote about watching an operator go to the tool store fourteen times in forty-five minutes, collecting one tool at a time. I’ve seen versions of that more often than I’d like to admit.

Searching. For the right spanner, the right insert, the drawing, the program, the forklift, the person with the key to the cabinet.

Waiting. For the crane, for quality to sign off a first off, for material nobody brought up because nobody knew the job was next.

Adjusting. Run a part, measure it, tweak, run another, measure again.

That last one is the big one, and it surprises people. Shigeo Shingo, the Japanese engineer most closely associated with quick changeover, broke a typical set up into four chunks. Preparing and checking tools and materials took about 30% of the time. Centring, dimensioning and setting conditions took about 15%. Trial runs and adjustments took about 50%. And actually mounting and removing the tool? Around 5%.

Five percent. The bit everyone pictures when they think “changeover” is barely a rounding error. The rest is preparation and guesswork.

A quick word on how you film it, because it matters. Tell people why you’re doing it. Make it clear you’re studying the process, not the person. The setter on that footage is usually the one who knows exactly where the time goes and has been quietly frustrated by it for years. Put them in the room when you watch it back, and let them talk first. You’ll learn more in an hour than in a month of stopwatch studies.

Then map it. List every step, how long it took and who did it. A simple spaghetti diagram, which is just a sketch of the machine with a line drawn wherever the operator walked, is brilliant for this. If it looks like someone’s dropped a plate of spaghetti on the drawing, well, you’ve found some easy wins.

Internal and external: the split that changes everything

Once you’ve got the list of steps, there’s one question to ask of every single one.

Does the machine have to be stopped to do this?

If it does, it’s internal set up. Taking the old tool out. Fitting the new one. A few genuine settings. That work can only happen when the process is stood.

If it doesn’t, it’s external set up. Fetching the tools. Finding the drawing. Bringing the material to the machine. Preheating a mould or die. Presetting tools off the machine. Checking you’ve got the right fixings. All of that can happen while the last job is still running.

The principle is simple, and it was the backbone of everything we did on the header machine. Do as much of the work as you can while the machine’s still running. Keep internal work to the absolute minimum, ideally just fitting and removing the tool, die or material, and nothing else.

I’d almost guarantee you’ll find that a lot of what’s being done with the machine stopped didn’t need the machine stopped at all. It’s just always been done that way. The setter stops the machine, then goes to look for the tooling. Nobody ever decided that was the right order. It just became the order.

Shingo described the journey in roughly four stages. First, make sure anything external really is done while the machine runs. Second, separate internal from external properly, so everyone can see which is which. Third, convert as much internal work as you can into external work. Fourth, improve everything that’s left.

Toyota’s big press changeovers are the classic example, and I think they’re worth knowing because they show how much of this is about preparation rather than clever engineering. Their huge stamping dies were being positioned by eye and nudged with crowbars, with test pressings in between, and a change could take anywhere from twelve hours to nearly three days. The first improvement was simply to record the right measurements for each die and set to those rather than by eye. That alone took it down to about an hour and a half. Then came staging the next die and the crane before the old one came out, and keeping the right tools at the press. Eventually it got to under ten minutes per die.

That’s where the name comes from. SMED stands for single minute exchange of die, but “single minute” means a single digit, so under ten minutes, not literally sixty seconds. Shingo usually gets the credit, though to be fair the history’s a bit more tangled than that, and Toyota’s engineers had been chipping away at changeover times since the forties. Shingo also claimed his own data showed set up times falling, on average, to around 2.5% of where they started. Maybe take that with a pinch of salt. But even a fraction of it would change most factories I know.

You can start moving work external without spending much at all:

Changeover kits or carts. Everything the job needs, tools, fixings, gauges and paperwork, staged at the machine before it stops.

A visible schedule. If the setter doesn’t know what’s next, they can’t prepare for it. A simple board showing the next two jobs fixes more than you’d think.

Preheating and presetting. Warm the mould, preset the tools, load the program, all while the current job finishes.

First off checks planned in. Agree with quality in advance when they’ll be needed, rather than waiting for someone to wander over.

Eliminate, combine, simplify

The phrase that’s stuck in my head since those early events is three words. Eliminate, combine, simplify.

It comes from a framework Toyota borrowed from the American Training Within Industry programme of the Second World War, usually written as eliminate, combine, rearrange and simplify. I’ve always remembered it as three, and to be honest three’s easier to keep on a whiteboard anyway.

Take whatever internal work is left and run each step through those words, in order.

Eliminate first. Can you stop doing this step altogether? Shingo had a lovely observation about bolts: it’s only the last turn that actually tightens it. Everything before that is just movement. So if a clamp needs twelve turns of a bolt, that’s eleven turns of waste on every changeover. Quarter turn fasteners, cam clamps, keyhole slots and quick release fittings all attack that. And do you really need eight bolts holding something that four would hold safely?

Adjustments are the other big target. Every adjustment is a sign that something isn’t located in the right place. Locating pins, fixed stops, spacers cut to height and marked datum lines can turn “fiddle until it’s right” into “fit it and it’s right.”

Then combine. Can two steps happen at once? Two people working in parallel, one each side of the machine, can sometimes halve what’s left of the internal time. It needs a bit of choreography, and you’ve got to think hard about safety, but it’s often worth it on a bottleneck machine.

Then simplify. Make whatever’s left easy and hard to get wrong. Standardise tool heights so everything sits at the same shut height. Use the same size fixing everywhere so one spanner does the lot. Colour code. Put a photo of the finished set up on the machine. Shingo called this standardising function rather than shape. Your tools don’t all need to be identical. They just need to fit and locate the same way.

A word of warning, from experience. Don’t start with the engineering. Teams love designing a clever quick release fixture, and fair enough, it’s the fun bit. But the cheap stuff, the cart, the schedule, the staging and the checklist, usually gets you a big chunk of the gain for very little money. Get that in first. Then spend engineering time on what’s left, once you can see what really matters.

On the header machine, if I remember rightly, a lot of our first day’s gains came from nothing more sophisticated than a trolley, a marker pen and a bit of agreement about who fetched what. The clever bits came later in the week.

Making it stick, and spending the time wisely

Here’s the frustrating part. A great SMED week can quietly unravel within a couple of months if nothing holds it in place. New setter, mad week, the cart gets borrowed for something else, and before you know it the machine’s stood while someone goes looking for an insert again.

A few things help.

Write the new standard down. A one-page changeover standard, ideally with photos, kept at the machine. Who does what, in what order, and what “ready” looks like before the machine stops.

Put changeover time on the board. If you’ve got a daily production board, add changeover time to it. What gets looked at every morning gets talked about. What gets talked about tends to hold.

Check the kit, not just the clock. A quick audit of the changeover cart once a week catches the slow drift before it costs you.

Go round again. A common rule of thumb is that each serious pass through the process takes out somewhere around 45% of what’s left. So a two-hour changeover might need a few rounds before it gets anywhere near ten minutes. That’s normal. It’s a loop, not a project.

Then there’s a question most teams forget to ask until it’s too late. What are you going to do with the time you’ve saved?

It’s tempting to keep running the same big batches and pocket the extra hours as output. Sometimes that’s the right call, especially if the machine’s a genuine bottleneck and the order books full. But often the bigger prize is changing over more often, running smaller batches, and taking stock and lead time out of the whole business. The hours you win back on the machine can come back to you as cash in the bank, space on the floor and shorter quotes for your customers.

I’d decide that on purpose, as a leadership team, rather than letting it happen by default. Otherwise, you tend to end up with neither.

Bringing it back to the header machine

Let’s pull it together.

Long changeovers do more damage than the minutes on the clock suggest. They push you into big batches, and big batches drive work in progress, finished stock, overproduction, waiting and endless moving of material. And with orders improving across UK manufacturing while hiring stays cautious, the capacity hiding inside your changeovers might be the cheapest capacity you’ll ever find.

The method isn’t complicated. Film a real changeover and watch it with the people who do it. Split internal from external, and move everything you can to while the machine’s still running. Then take what’s left and eliminate, combine and simplify. Standardise it, measure it daily and go round again.

Think back to that customer pushing us to buy another header machine. We never needed it. The capacity was there all along. It was just spending a whole shift at a time getting ready to work.

So before you sign off on new kit, film your worst changeover. You might be surprised. I usually am, even now.

If you’d like a hand, this is exactly the kind of thing we do at TCMUK. Our Lean Coaching and Mentoring Programme trains your own people in tools like SMED and then coaches them through live projects on your shop floor, so the gains belong to your team and keep coming long after we’ve gone. You can read more about the Lean Coaching and Mentoring Programme, or book a 15 minute call with Adam to talk through the changeover that’s causing you the most grief. No pitch. Just a conversation about whether we can help. Your machines are probably far more capable than your changeovers are letting them be.

0330 311 2820

Book a Return Call at a time that Best Suits You “HERE”